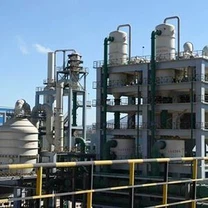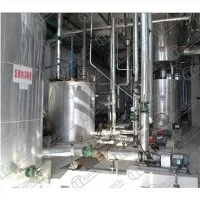


Asia Pacific Chemical Factory Co., Ltd. has always been committed to providing high-quality products and solutions in the chemical industry. Recently, we are proud to announce the launch of a new phosphoric acid pilot plant to meet growing customer demand. The establishment of this pilot factory will bring unique advantages to the Asia-Pacific region and enable us to provide more innovative products and services.
This phosphoric acid pilot plant was established to meet growing market demand and continue innovation in the chemical industry. As an important chemical raw material, phosphoric acid is widely used in many fields, including food and beverages, fertilizer production, metal processing, etc. Our pilot plant will be dedicated to producing high-quality phosphoric acid to meet the needs of various industries.
This pilot factory will use the most advanced production technology and equipment to ensure consistency and stability of product quality. We will strictly comply with all relevant environmental regulations and adopt sustainable production practices to reduce environmental impact. This is in line with Asia Pacific Chemical Factory Co., Ltd.'s consistent commitment to sustainable development and will help reduce our carbon footprint and protect our environment.
In addition, our phosphoric acid pilot plant will provide customized solutions to meet customers' specific needs. We will actively participate in R&D and innovation to develop new phosphoric acid applications and provide customers with more choices. We believe that through continuous innovation, we can create a better future together with our customers.
Asia Pacific Chemical Factory Co., Ltd.'s phosphoric acid pilot plant will become an important part of our growing product portfolio, providing customers with more high-quality chemical products. We look forward to working with you to explore the unlimited potential of phosphoric acid and bring more innovative solutions to various industries. We firmly believe that through cooperation, we will be able to achieve a win-win situation and make greater contributions to the chemical market in the Asia-Pacific region.

Technological innovation: The company has advanced chemical equipment and processes, and constantly develops new products and improves existing products. The company also cooperates with a number of domestic and foreign scientific research institutions and universities to introduce and develop new technologies and knowledge to improve product quality and performance.

Market competitiveness: The company's products cover multiple fields and industries, such as agriculture, medicine, chemical fiber, dyes, plastics, rubber, etc. The company's products enjoy a good reputation and credibility in domestic and foreign markets, and it has established long-term cooperative relationships with many well-known customers. The company also actively explores new markets and customers to increase product sales and revenue.

Environmental responsibility: The company pays attention to environmental protection and resource conservation, and adopts a variety of measures, such as recycling, wastewater treatment, exhaust gas purification, solid waste disposal, etc., to reduce environmental pollution and impact during the production process. The company also actively participates in social welfare activities, supports local education, medical, cultural and other undertakings, and fulfills its corporate social responsibility.